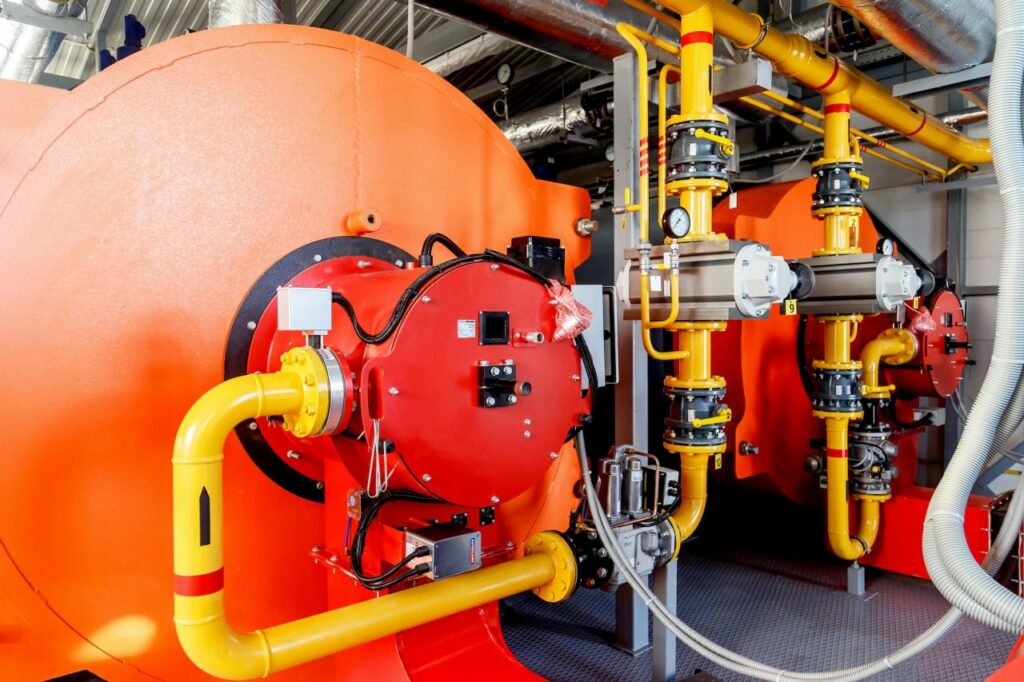
Selecting a burner for industrial heating is often treated as a capacity exercise: calculate the required heat input, find a model in the right range, and check the fuel. That works for many installations, but it breaks down when the process imposes conditions that a catalog configuration cannot comfortably meet.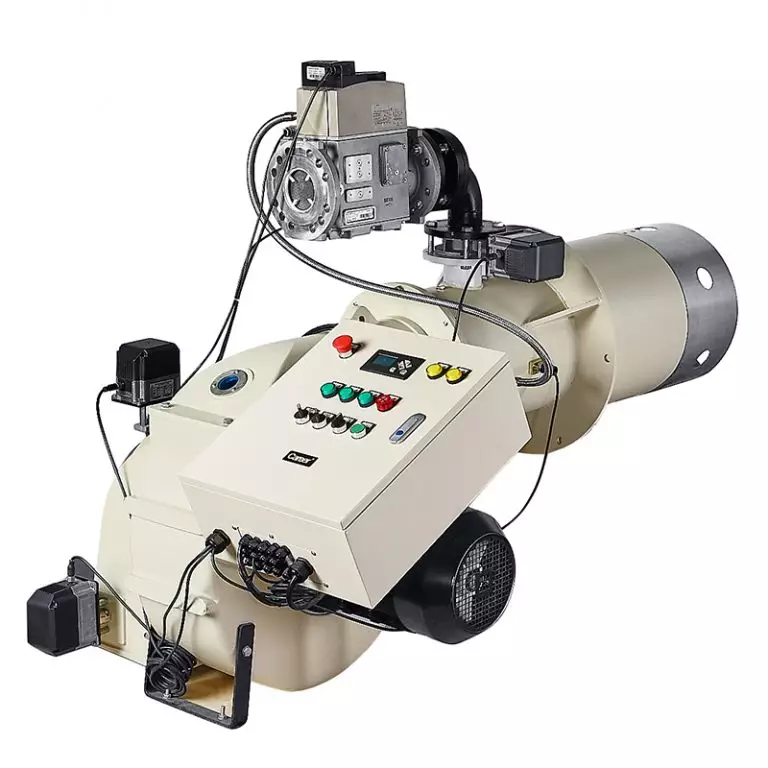
Customization becomes essential when standard hardware falls short—whether that means accommodating an unconventional chamber shape, tracking a volatile load profile, managing complex fuel arrangements, hitting strict emission targets, or navigating a tight retrofit constraint.
Capacity Is Only the First Filter
Heat input tells us how much energy the burner must deliver. It does not tell us where that energy should be released, how the flame should behave, or how consistently the burner must follow changing demand.
A long furnace may require a different flame geometry from a compact chamber. Direct-fired equipment may need carefully controlled heat distribution, while an immersion-tube system has a completely different combustion arrangement.
If those elements already align with a proven catalog configuration, there may be little reason to customize.
The Strongest Case for Customization Is a Specific Mismatch
Custom burners become defensible when an existing configuration cannot meet a known requirement cleanly. Chamber geometry is one common trigger. A flame that is too long, too short, or poorly positioned can create unwanted temperature patterns even when the rated capacity is correct.
Load behavior provides another signal. Some processes move rapidly between high and low firing rates, making modulation range more significant than maximum output alone. Our BX20 immersion tube burner, for example, is listed with a 40:1 turndown ratio and is intended for applications requiring dynamic heat adjustment.
Fuel conditions can create a third mismatch. Natural gas, LPG, biogas, oil, methanol, and waste-oil systems do not automatically call for identical combustion arrangements. Fuel pressure, delivery method, viscosity where relevant, and the required control strategy all need to be established before deciding whether a standard configuration is suitable.
Emissions can be the deciding factor as well. If a project has a defined NOx target, combustion design may need to accommodate technologies such as flue-gas recirculation rather than treating emissions as a final-stage adjustment. We list an NX low-NOx FGR series with NOx below 30 mg/Nm³ under its stated conditions.
The Engineering Brief Should Describe the Whole Combustion Envelope
A useful customization request begins with process information, not a preferred burner model. We would want the required heat input and operating range, fuel type and supply conditions, combustion-chamber dimensions, installation position, control signals, and emissions requirements.
The low-fire requirement deserves particular attention. A burner sized only around maximum demand can still be poorly matched if the process spends substantial time at reduced load. Turndown, ignition behavior, flame stability, and control response should be considered together.
Physical integration also matters. A retrofit may involve an existing burner opening, limited service space, fixed electrical characteristics, or an established control panel. We at Career Burner state that we can tailor burners for different fuels and processes, including high-turndown, staged-combustion, and variable-load applications, as well as certain 12/24VDC and 60Hz configurations.
For industrial burner manufacturers, application data separates useful engineering from simply offering a larger or smaller unit. We expect industrial burner manufacturers to use that information to evaluate the complete combustion system.
A Standard Burner Wins Whenever the Requirements Already Fit
Custom burners should not become a default purchasing requirement. If a standard burner already matches the fuel, capacity, flame arrangement, installation interface, control requirements, and operating range, it can be the more sensible engineering choice.
The GX25 illustrates this situation. It supports natural gas and LPG, offers single- or multi-stage flame modulation, and includes flame detection and pressure monitoring. The manufacturer lists it for boilers, ovens, and food-processing equipment.
A standard solution can also simplify replacement and commissioning because the equipment configuration is already established. Customization is most valuable when it solves a measurable problem; adding unique features without a process-driven reason can complicate engineering without improving the result.
That distinction is especially useful during retrofit projects. We would compare the existing interface and process conditions against available standard models. Sometimes the right answer is a standard burner with an appropriate configuration rather than a newly engineered combustion package.
Turn the Decision Into a Requirement Test
A practical decision can be reduced to one question: does the process contain a requirement that an existing burner configuration cannot satisfy without compromise?
If the answer concerns flame geometry, unusual chamber dimensions, exceptional modulation needs, fuel characteristics, emissions performance, controls, or physical integration, customization deserves technical evaluation. If none of those areas creates a meaningful mismatch, a standard product is usually the more proportionate route.
At Career Burner, we engineer application-specific solutions with a complete burner range covering gas, oil, methanol, waste oil, and low-NOx technologies.
The best customized solutions are therefore not defined by how different they look from catalog equipment. They are defined by how precisely they solve a documented process requirement. We recommend starting with operating data, identifying the actual mismatch, and customizing only the elements that need to change. That keeps the combustion system technically purposeful while avoiding unnecessary complexity.