- No. 3 Nanhua Industrial Road Xingtan town, Shunde District ,Foshan City, Guangdong Province, China
- sales@careerburner.cn,junnymai@careerburner.cn
- +86-13690622890
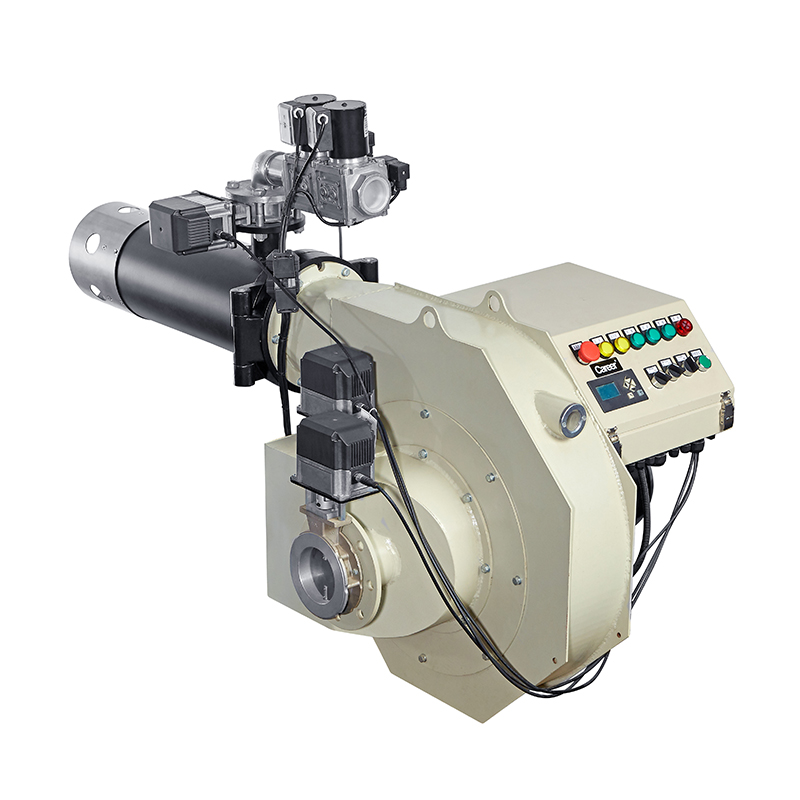
Career Low NOx Gas Burners– Designed for Efficient, Eco-friendly Performance
Career Burner’s low NOx gas burners are engineered for industrial and commercial heating systems that require efficient combustion with reduced nitrogen oxide emissions. Using optimized air-fuel mixing and advanced low NOx burner technology, Career’s low NOx gas burners deliver high efficiency and low NOx emissions up to ≤30 mg/Nm³, with a capacity range of 700-3300 kW.
Designed for industries such as boilers, incinerators, and food processing, these burners offer clean combustion, energy savings, and environmental compliance. Compatible with natural gas and LPG, each FGR burner recirculates part of the flue gas to lower peak flame temperatures, supporting stable combustion, efficient operation, and reduced NOx emissions.
Contact us today for a quote or a customized low-emission combustion solution for your application.

Low NOx gas burners reduce NOx emissions by carefully controlling the combustion process-typically by mixing fuel and air more thoroughly, lowering the flame temperature, and sometimes recirculating flue gases. These techniques limit the formation of nitrogen oxides, which are mainly produced at high temperatures when nitrogen and oxygen in the air combine.
Different applications require different low NOx burner technologies. Common solutions include:
Ultra-Low NOx burners are advanced industrial burners designed to reduce nitrogen oxide emissions to extremely low levels—typically below 15 ppm. An ultra-low NOx gas burner typically uses precise air-fuel control and advanced combustion technology to achieve these reductions. Zero NOx burners, on the other hand, represent emerging technologies that eliminate NOx emissions entirely by avoiding flame-based combustion, using methods like electric heating, hydrogen fuel, or plasma-assisted systems, making them ideal for zero-emission manufacturing and net-zero industry initiatives.
Our Flue Gas Recirculation (FGR) technology delivers NOx ≤30mg/Nm³
Absolutely. Our burners support natural gas and LPG fuels, and can be tailored for high-turndown, staged combustion, or variable load applications based on your requirements.
Career low NOx burners can be configured for industrial boilers, food-processing heating equipment, and textile heat-recovery systems. Final suitability depends on the required heat output, combustion-chamber design, fuel conditions, operating load, and applicable NOx emission limits.
Career Burner provides a standard 18-month warranty from the date of arrival at destination port, extendable through a service agreement that includes preventive maintenance, on-call technical support, and spare parts supply.
The estimated lead time is 45 days from order confirmation, with DDP or DAP shipping terms available. Upon order confirmation, we’ll provide a more accurate estimated schedule for you.